Whiplash Industrial

Charleston, South Carolina

Develop it.
Wire it.
Weld it.

In-house R&D and product development, PLC and HMI controls integration, and robotic and heavy weldments, from first prototype to production run.

Whiplash Industrial. Precision under pressure. Made in U.S.A.
R&DProduct development in house
PLC/HMIControls integration
RoboticFANUC arc welding cell
250,000 lbLoad-tested lifting adapters, NASA Stennis

What we do

From first idea to production run

Most of what leaves here was developed, prototyped, machined, welded and wired without crossing a property line. Fewer handoffs, fewer surprises, one company answering for the whole machine.

01 / DEVELOPMENT

R&D and product development

Bring a problem, a sketch or a half-finished design. We develop it with you, then build the mockups and first articles in the same shop that builds the production run.

  • Concept design and engineering
  • Prototypes and mockups
  • Design for manufacture before anything runs in volume
  • Custom solutions for problems nobody sells a fix for
02 / CONTROLS

PLC & HMI controls integration

Controls designed alongside the machine rather than bolted on after it, so the panel, the program and the steel arrive as one system.

  • PLC programming and HMI screens
  • Control panel build and wiring
  • Integration with the equipment we build
  • Controls for custom machines and skid packages

03 / WELDING

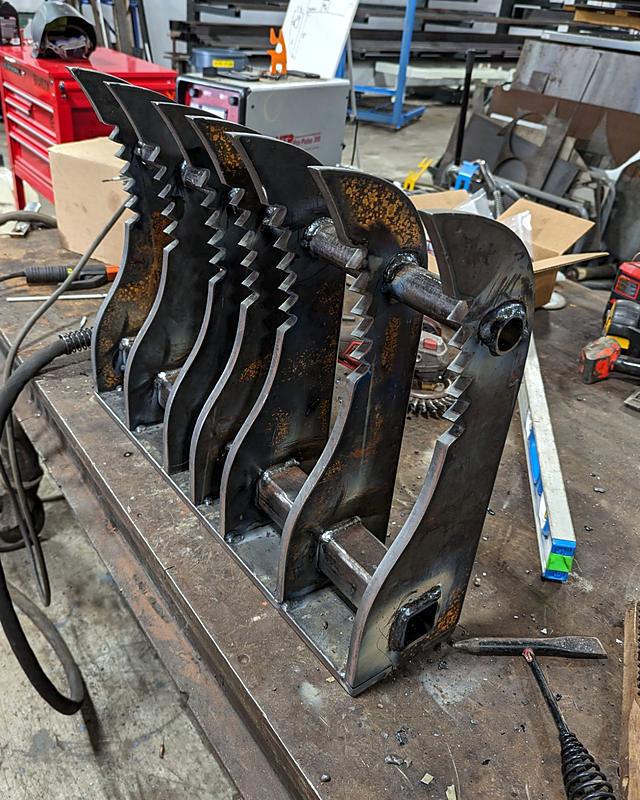
Robotic & heavy weldments

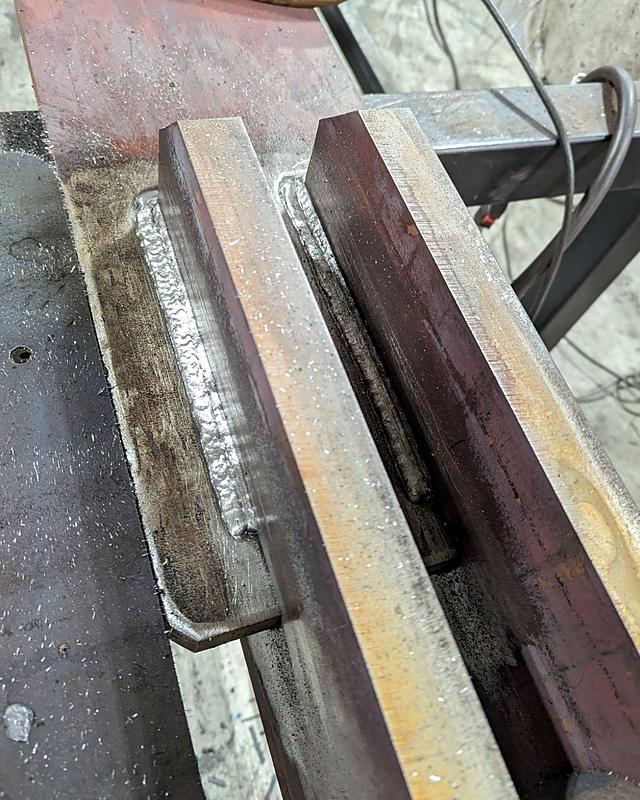
A FANUC robotic arc welding cell for repeat work, and fixtured manual welding for structural frames too big or too heavy for most shops.

  • Robotic MIG welding
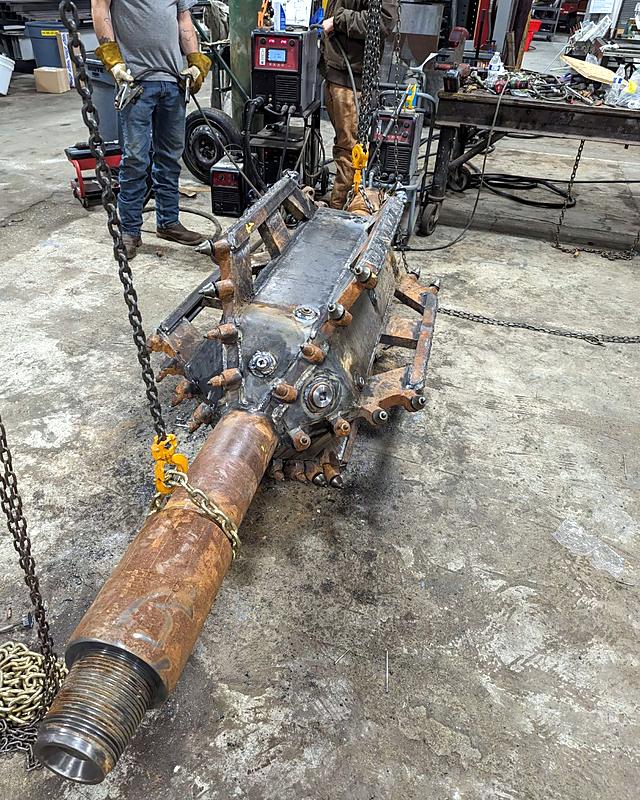
  • Heavy structural weldments, assemblies past 30,000 lb
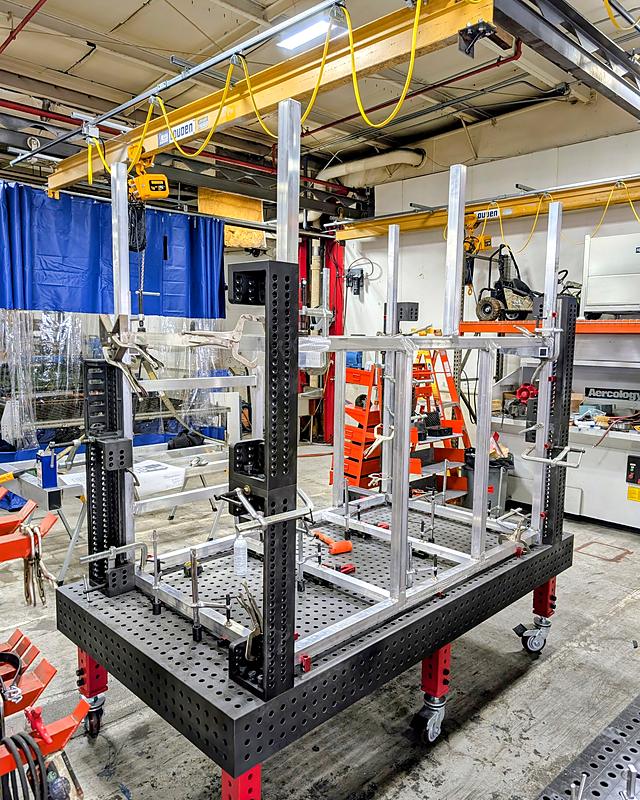
  • Precision fixturing for frames and jigs
  • MIG, TIG and flux-core to written procedures

04 / MACHINING

CNC machining

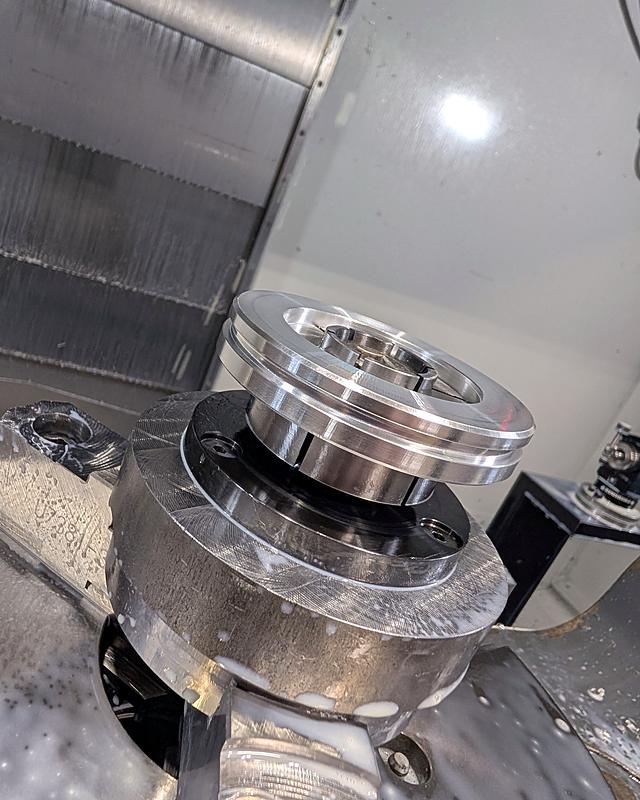
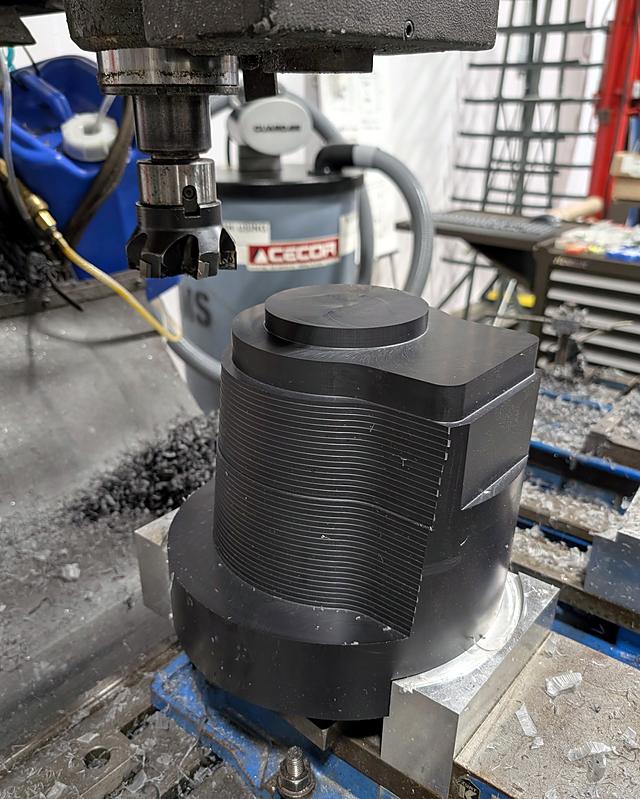
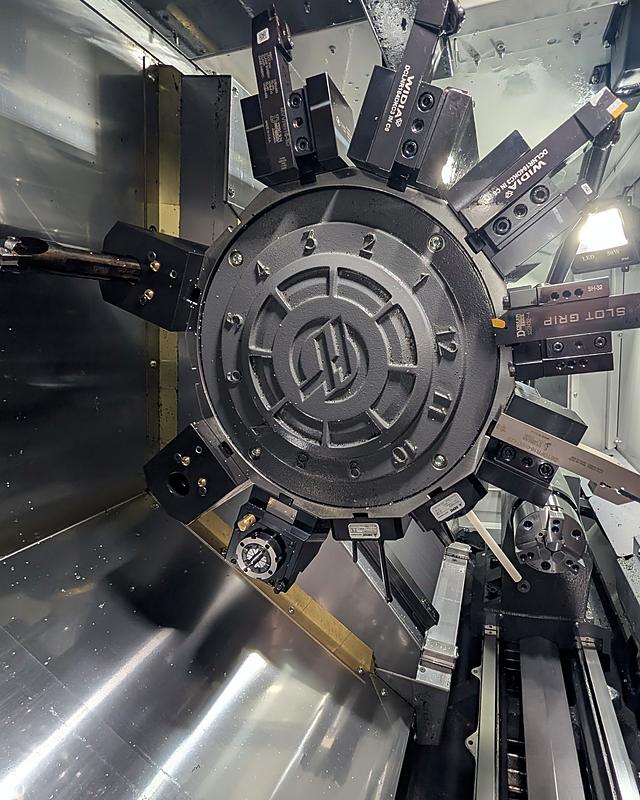
Five-axis milling on a 50-taper trunnion machine and turning with live tooling and a Y axis, so most parts finish complete in one or two setups.

  • Prototype through production runs
  • Machined-after-weld work
  • Threading, tapping and NPT port work
  • Carbon, stainless, aluminum, tool steels and plastics

05 / TOOLING

Custom tool & die

Punches, dies and forming tools made in house, for our own production and for yours.

  • Punch and die sets
  • Forming and bending tools
  • Tooling designed together with the part it makes

06 / PRODUCTION

OEM & contract manufacturing

Your product, built to your drawings on a repeating schedule, with the cutting, bending, forming and assembly done here.

  • Multi-unit production runs
  • CNC plasma cutting, press brake bending and forming
  • Mechanical assembly, hardware and rivet-nut installation
  • First-article documentation on production sets

07 / ON SITE

Field services

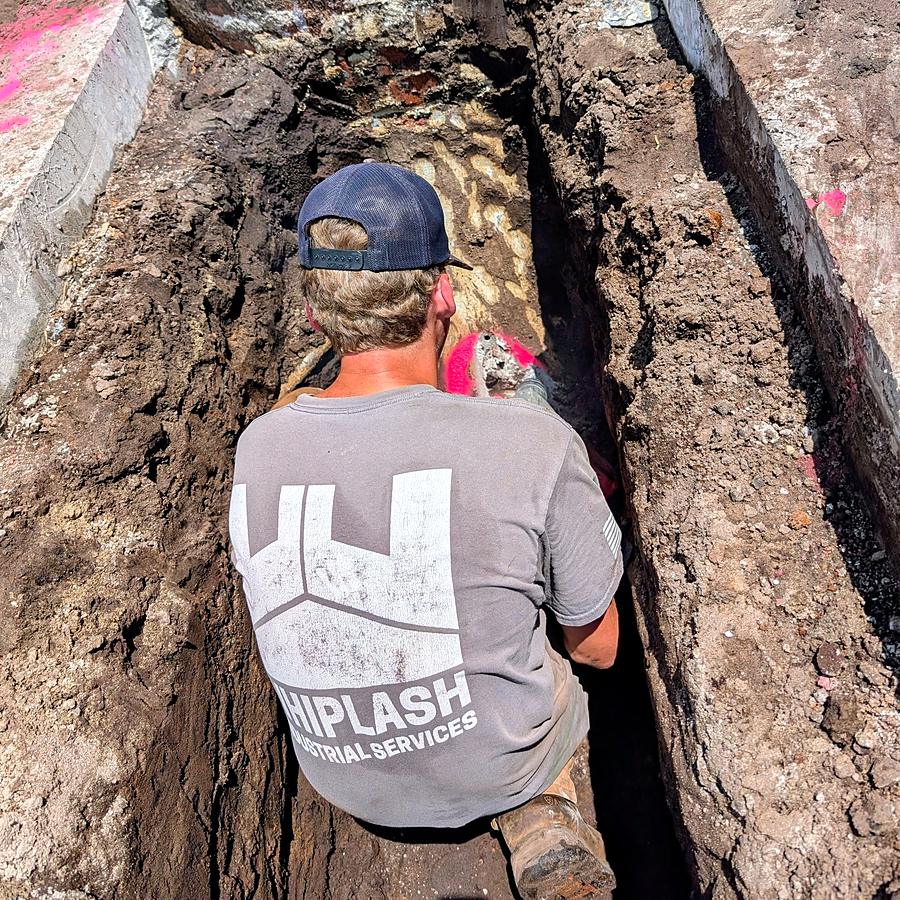
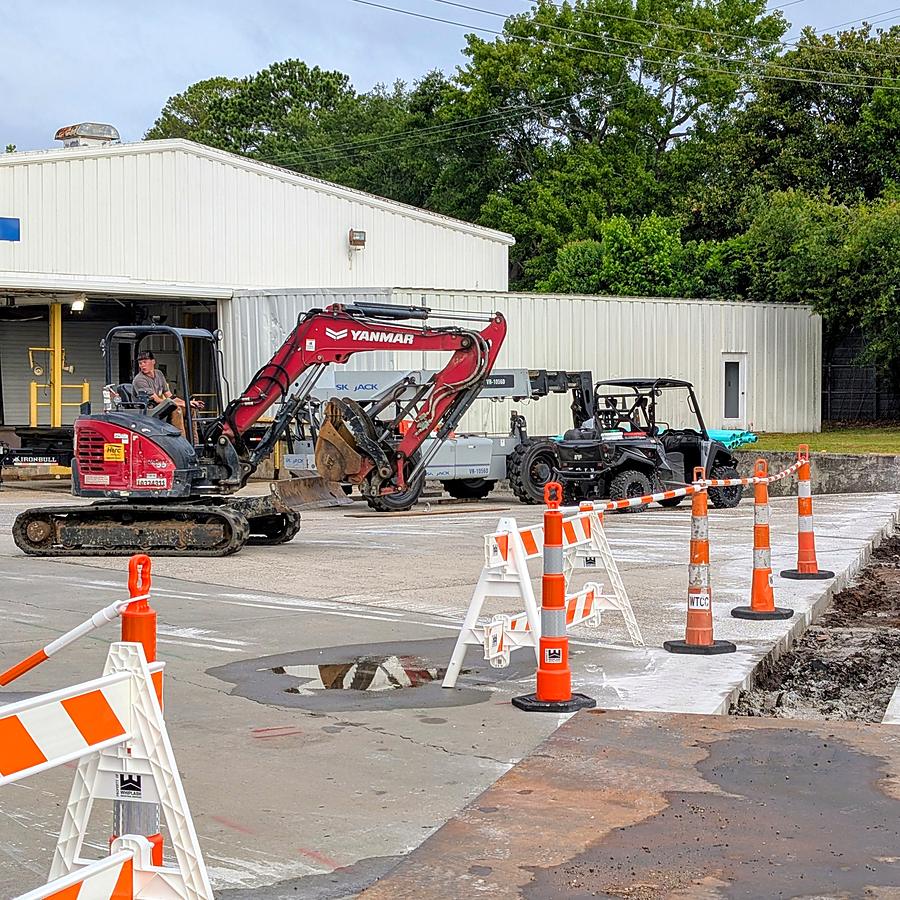
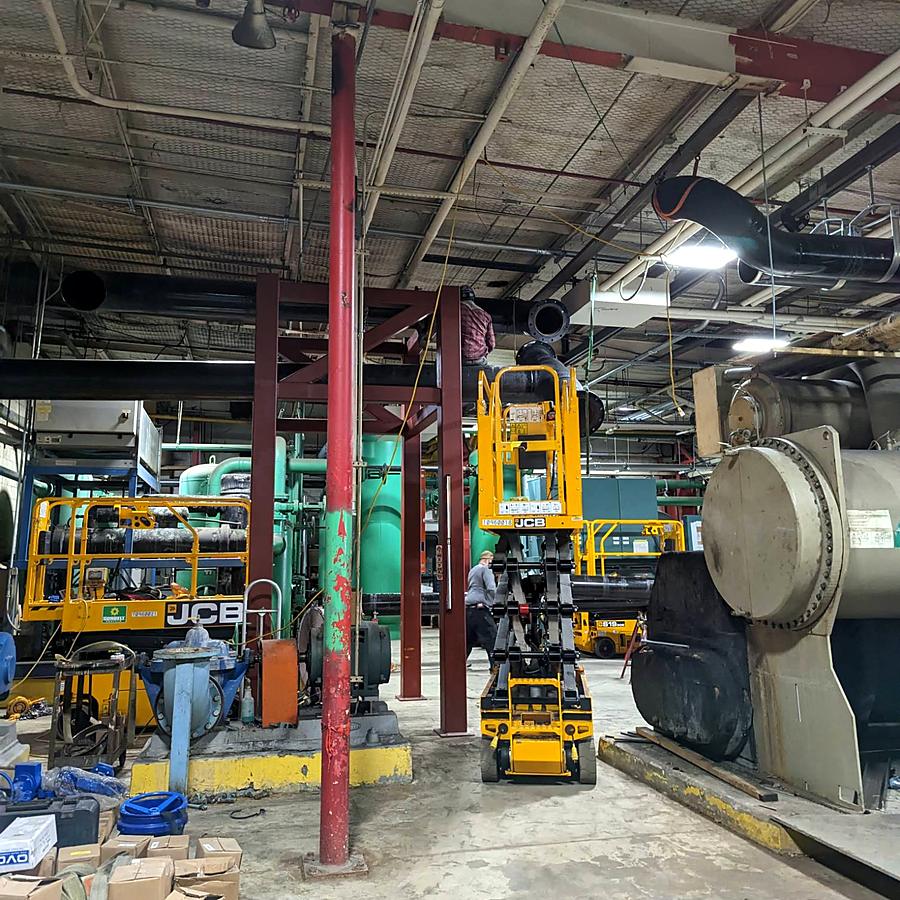
When the work cannot come to the shop, we take the shop to it.

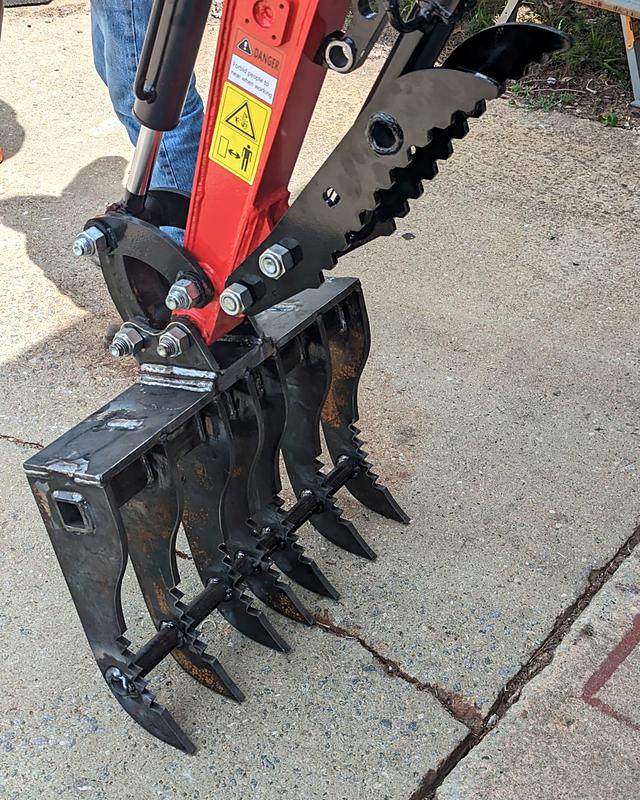
  • On-site fabrication
  • Retrofits & upgrades
  • Demolition
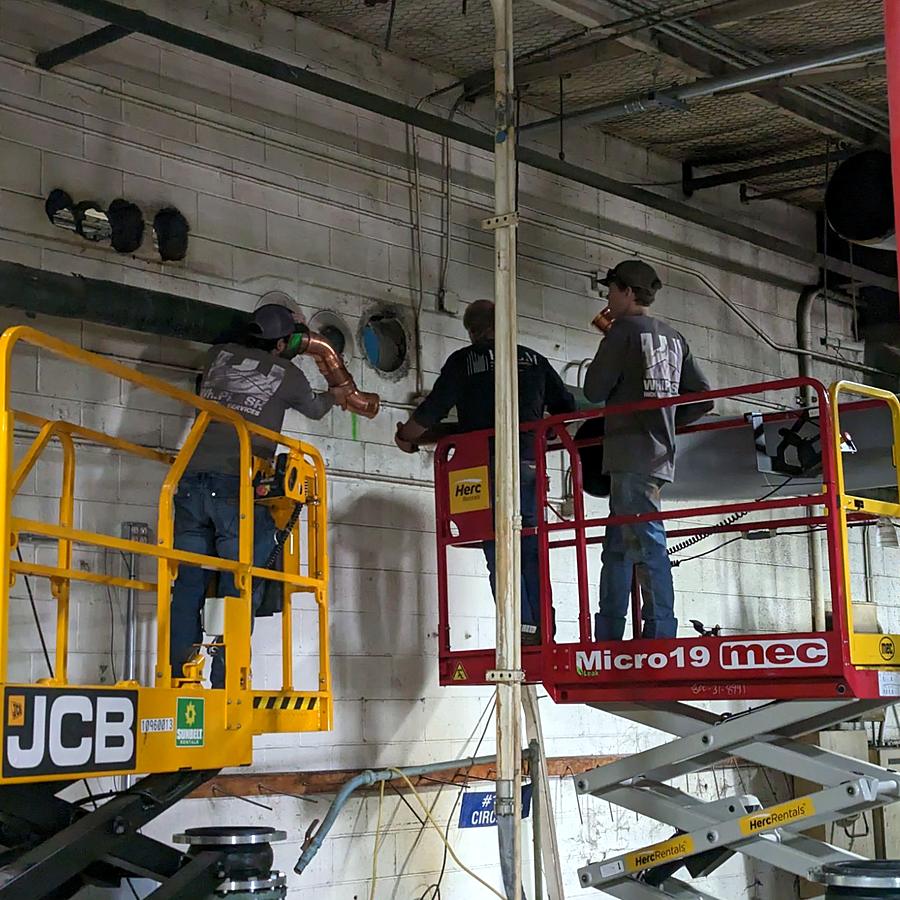
Our crew fitting copper piping from scissor lifts inside a plant A Whiplash Industrial Services crew member working in a trench Site work: a mini excavator beside a trench cut through concrete, coned off New pipe support steel in a plant mechanical room

Flagship work

Built for the parts that are too big for most shops

Complete structural skid packages: frames, bases, racks, covers and grating, built as a repeating production set rather than a one-off. Long beams, heavy plate and hundreds of tapped holes per unit.

The work that defines the shop is large structural weldments assembled into finished skids. Frames run past twenty-two feet, which puts them beyond the envelope of a typical job shop saw.

Repeat sets are built on precision fixturing rather than on layout, so unit two matches unit one and the labor curve actually comes down. Beam that exceeds our saw envelope is bought cut to length from the service center and detailed here, which keeps a long part from becoming an impossible in-house cut.

Copes, chamfers and tap-drilled holes stay in house. Tapped holes are drilled rather than thermally cut, because work-hardened edges do not tap cleanly, and hardware locations are chased after galvanizing where the spec calls for it.

Demonstrated envelope
Longest frame built22 ft 10 in
Heaviest finished assemblyOver 30,000 lb
Heaviest single weldmentApprox. 5,300 lb
Structural shapesThrough W16 and heavier
In-house saw envelope12.5 in × 12.5 in
Longer stockCut to length by the service center
PlateA36, pickled and oiled where offered
SheetHot rolled, pickled and oiled
StructuralA992 shapes, HSS
Production cadenceMulti-unit sets, scheduled
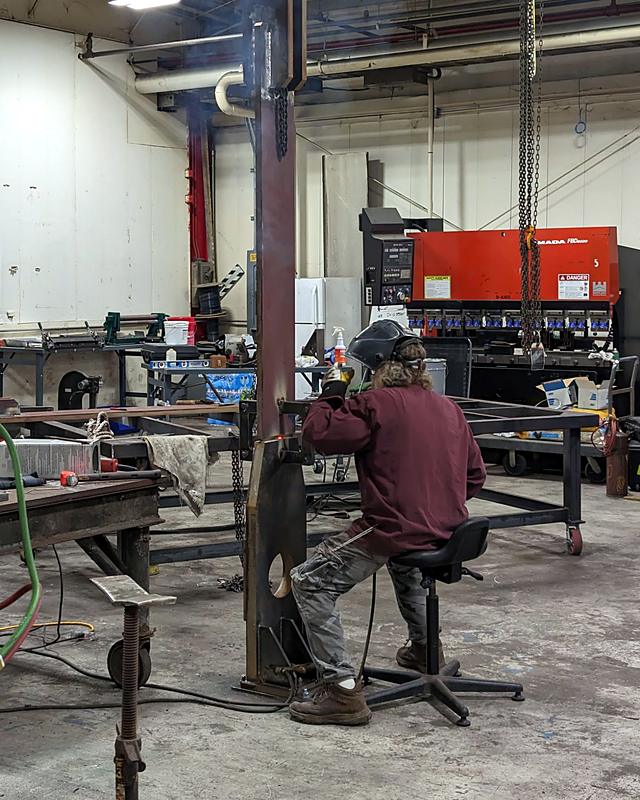
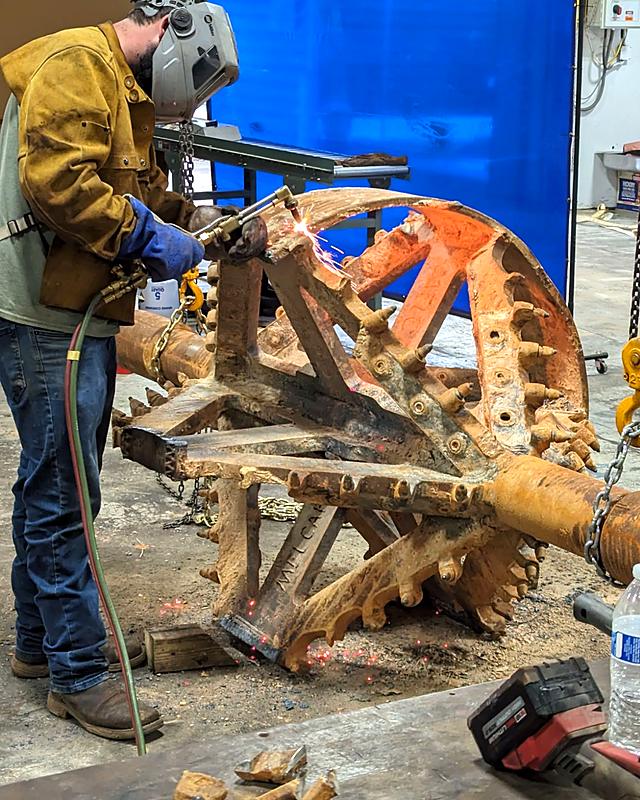
One of the nine lifting adapters being welded while it hangs from a chain hoist, a press brake behind
Welding one of the nine
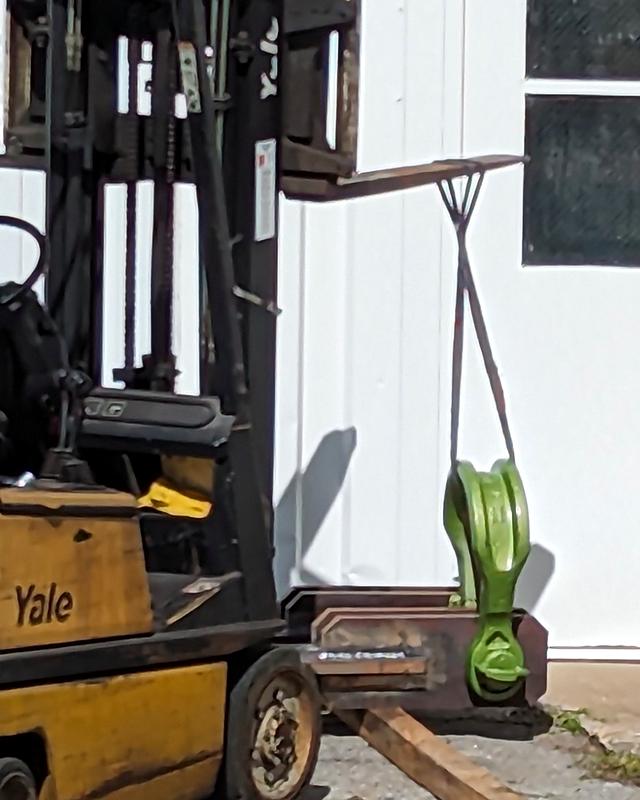
A forklift holding the adapter's giant green shackle on its plate
The shackle that connects it to the crane
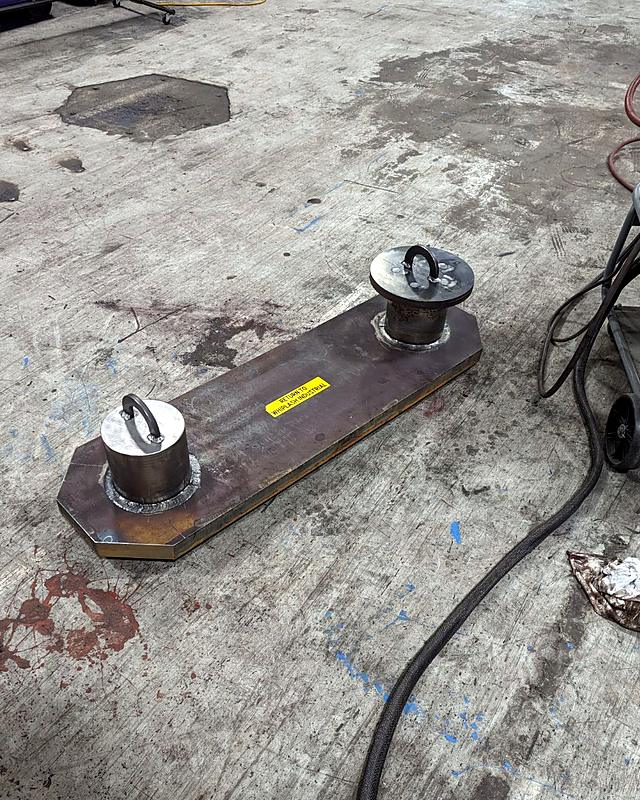
A heavy plate fixture with two lifting pins, labelled Return to Whiplash Industrial
The fixture we designed and built for the load tests

PROJECT / NASA STENNIS SPACE CENTER

Below-the-hook lifting adapters, load tested to 250,000 lb

Nine adapters, each about nine feet tall, built for removing rocket fuel tanks at NASA's John C. Stennis Space Center in Mississippi. Every one was load tested to 250,000 lb, and all nine passed the first time.

We also designed and built the fixture for the load tests, so the test facility could attach its slings to the adapters safely.

Units built9
Load test250,000 lb, each unit
ResultAll nine passed, first time
HeightAbout 9 ft
Used atNASA Stennis Space Center, Mississippi
Test fixtureDesigned and built here for safe rigging at the test facility

Recent work

Off our own floor

Every photo on this page is from our own jobs: in the shop, on site and in the plant.

Equipment

What is actually on the floor

The real list, not a capability brochure. If a machine is named here it is installed and running.

Machining

  1. Haas VF-6/50TR5-axis VMC · 50 taper · trunnion
  2. Haas ST-28YTurning center · Y axis · live tooling
  3. CNC knee mill3-axis
  4. Manual lathe13 in swing
  5. Manual lathe, circa 191324 in swing · restored in our shop
  6. Haas HAB-3232Automatic bandsaw · 12.5 in × 12.5 in

Cutting & forming

  1. CNC plasma cutting table5 ft × 10 ft · plate to 1 in
  2. Oxy-acetylene torchesTorch cutting
  3. Amada press brakes × 280 ton and 125 ton · 1/4 in plate, single bends over 10 ft long
  4. Betenbender press brake50 ton
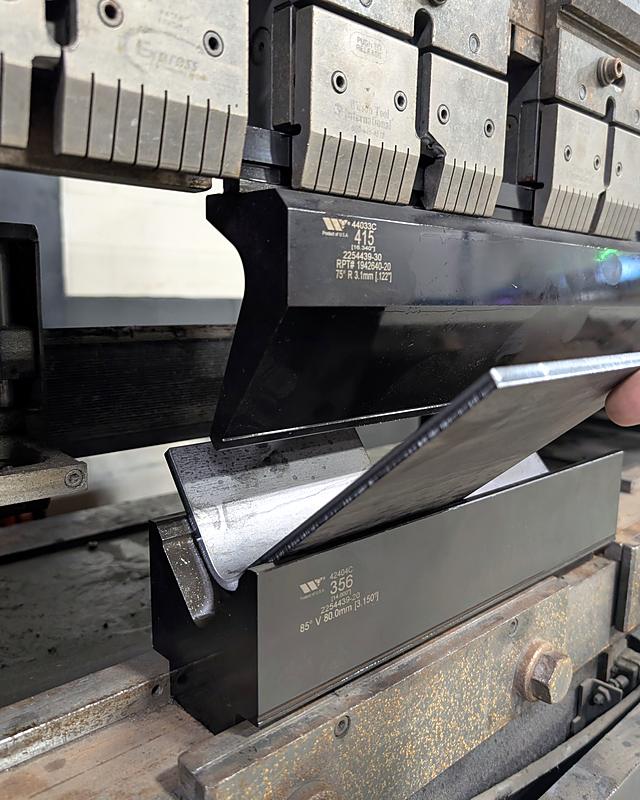
  5. Press brake tooling75°, 85° and 88° · V dies 1/4 in to 3.5 in · extra-large goosenecks and straight punches
  6. Baileigh WR-105V-ATCCNC router · 5 ft × 10 ft · tool changer

Welding

  1. FANUC ARC Mate 120iB robotR-30iA controller · 65.6 in reach · 44 lb payload
  2. Lincoln Power Wave 455MRobotic MIG power source · PowerFeed 10R
  3. Fireball Tool HD fixture tables × 2Cast iron · precision-tolerance fixturing
  4. Cast tower block fixturingRepeatable setups for frames and jigs
  5. MIG, TIG and flux-core stationsWelded to written procedures

Inspection

  1. FARO Focus S703D laser scanner · as-built verification
  2. Magnetic particle testingMT · surface cracks in welds and steel
  3. Ultrasonic thickness gaugeUT · plate and wall thickness
  4. MicrometersUp to 12 in
  5. Bore gaugesUp to 12 in
  6. Mitutoyo digital calipers0 to 8 in · coolant resistant
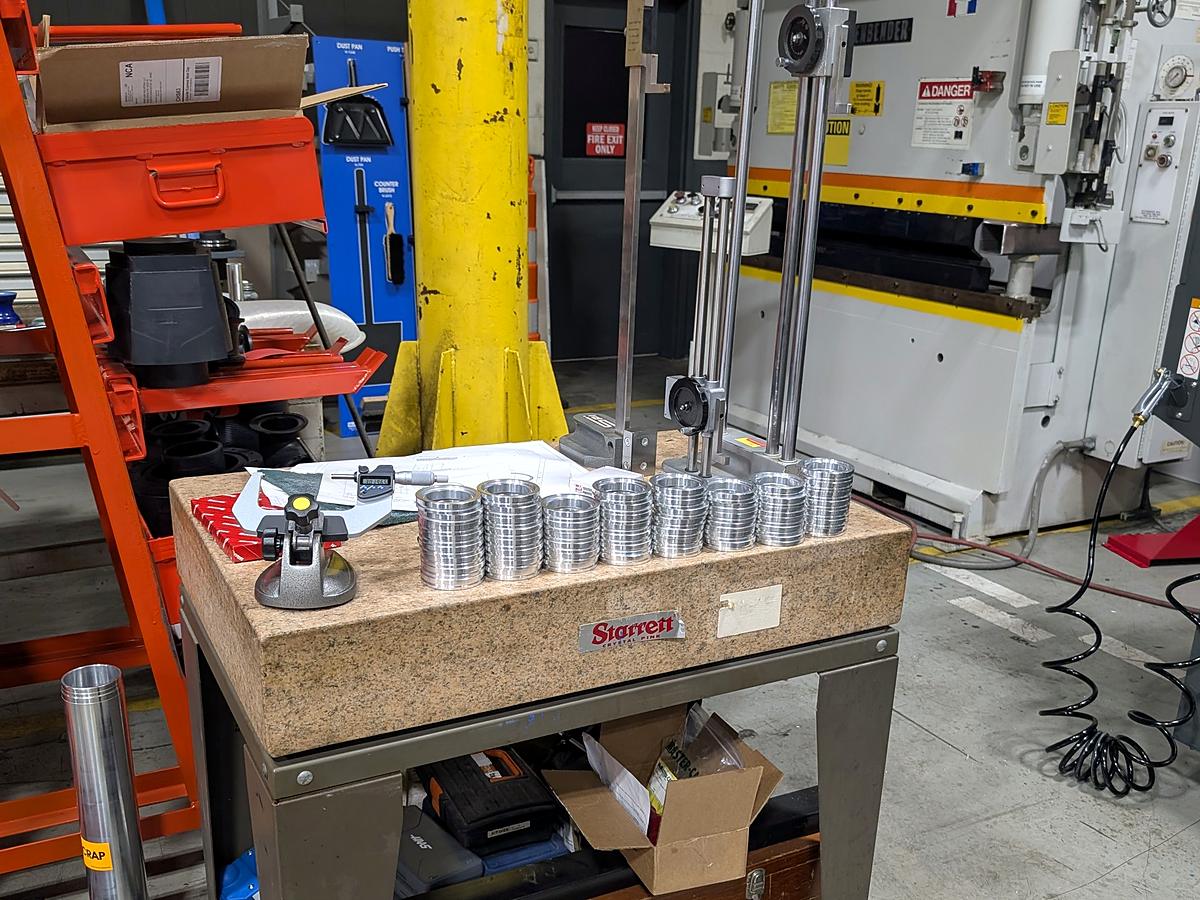
  7. Granite surface plateHeight gauge · layout and inspection
  8. Calibrated thread ring gauge3 in NPT · with certificate
  9. And the rest of the metrologyAsk for the full list

Material handling

  1. Overhead bridge cranesCeiling mounted · throughout the shop
  2. Skyjack VR-1056D telehandlerRough terrain · yard and load-out
  3. RiggingHoists · chain and nylon slings · shackles · loads to 30,000 lb
  4. Machine rollersRelocating machinery up to 120,000 lb

Casting & forging

  1. Burnout furnaceNatural gas · 30 in cube · up to 2,400 °F · PLC temperature control for burnouts and heat cycling
  2. Electric melting pot480 VAC three-phase · casting
  3. Propane forgesForging

Quality

Measured, documented, traceable

Inspection is a step in the router, not a favor at the end. What gets measured and what gets recorded is agreed before the first cut.

Dimensional verification

Long weldments are scanned rather than tape-measured. A laser scan of a finished frame compares the as-built against the model, which is the only practical way to prove a twenty-foot weldment landed where the drawing said.

  • FARO Focus S70 laser scanning
  • Micrometers and bore gauges up to 12 in
  • Calibrated hand metrology with certificates
  • First-article documentation on production sets

Nondestructive testing

Magnetic particle inspection and ultrasonic thickness gauging are done in house, so welds and wall thickness are checked without the part leaving the building.

  • Magnetic particle (MT) inspection of welds and steel
  • Ultrasonic (UT) thickness gauging of plate and wall

Material traceability

Mill test reports and domestic melt confirmation are available where the job requires them. Where a spec calls for US-sourced steel we buy to it and keep the paper.

  • Mill test reports on request
  • Domestic melt and pour where specified
  • Heat numbers retained against the work order
  • Parts marked and traced through every step of fabrication
  • Zebra TC22 handheld scanners throughout the shop
  • Our own in-house manufacturing and shop floor management system
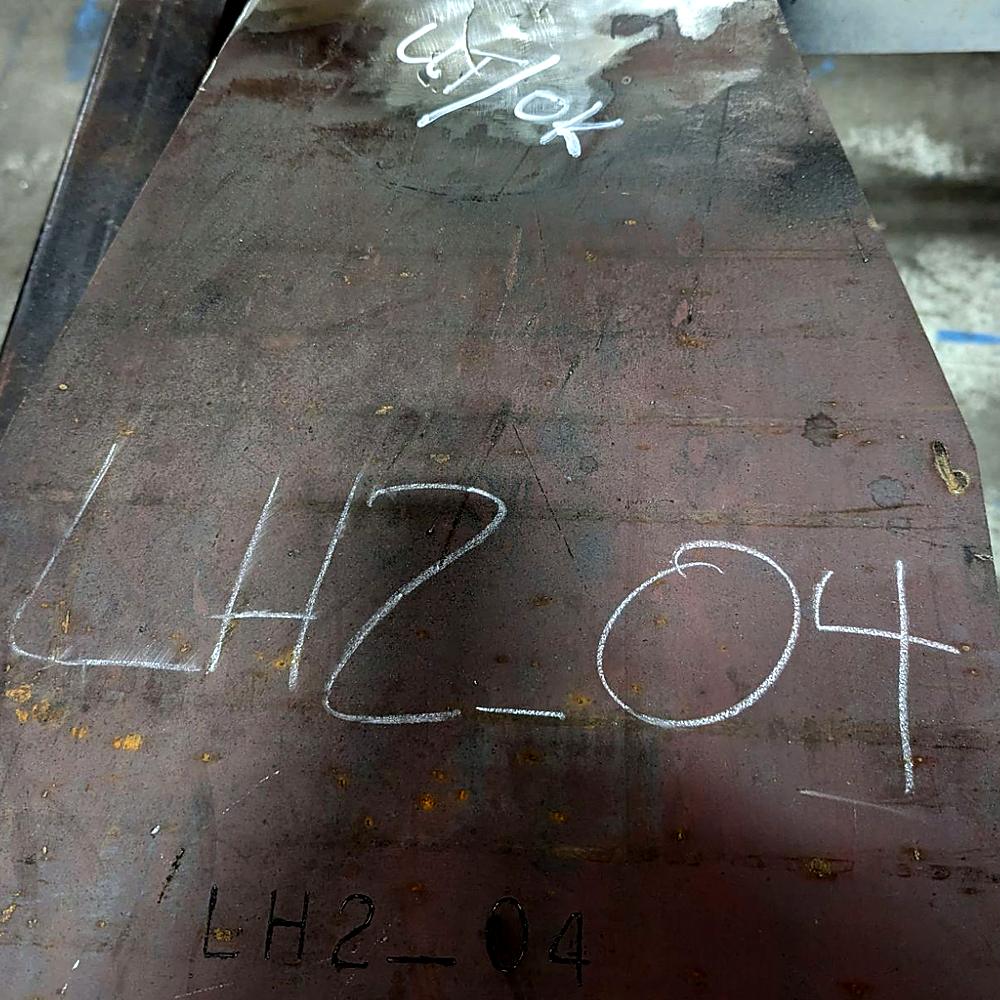
Part LH2_04, its number etched in and chalked on, its weld marked UT OK
LH2_04, a part for the NASA Stennis liquid-hydrogen lifting adapters: number etched and chalked, weld signed off after ultrasonic testing (UT OK). Traceability follows every part through the whole fabrication process, for quality assurance.
Machined parts checked with a height gauge on a granite surface plate

How it runs

From your idea to our dock

Bring the problem

A sketch, a problem statement or a full drawing package with a STEP model. We start wherever you are.

Develop and prove it

Concept, prototype and mockup, with the controls designed alongside the steel. You sign off on a first article before anything runs in volume.

Questions, then a number

Every part is counted off the model, nested and priced against live material quotes. Conflicts and gaps come back as written questions before anything is ordered.

Build, program, inspect

Machine, form and weld on precision fixturing or the robot, wire and program the controls, and inspect at the points agreed in the quote.

Contact

Tell us what you need built

Send a drawing package, or just the problem, and we will come back with questions, a plan and a number.

Send us your drawings

A drawing package, a STEP model, photos or a description of the problem all work. Part count, sizes, material, quantity and target date help us come back faster.

Entity
Whiplash Industrial LLC
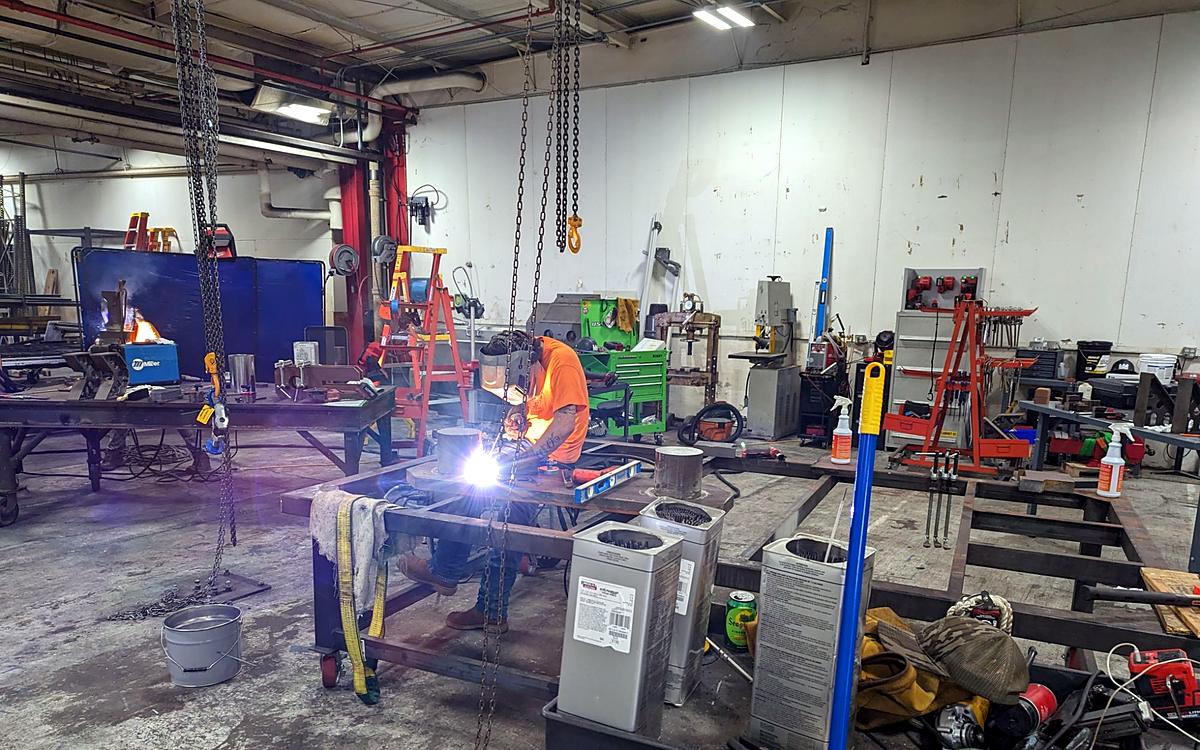
The shop floor, with welding underway at the tables